


Our Possibilities
From refined recipes and precise laboratory work to large-scale production and reliable warehousing — everything your brand needs under one roof.
Full support – from
recipes for delivery
 A laboratory that creates innovations – Each recipe is perfect, refined down to the last detail.
Production on your terms – Up to 250 tons per month, created exactly as you want as you need it.
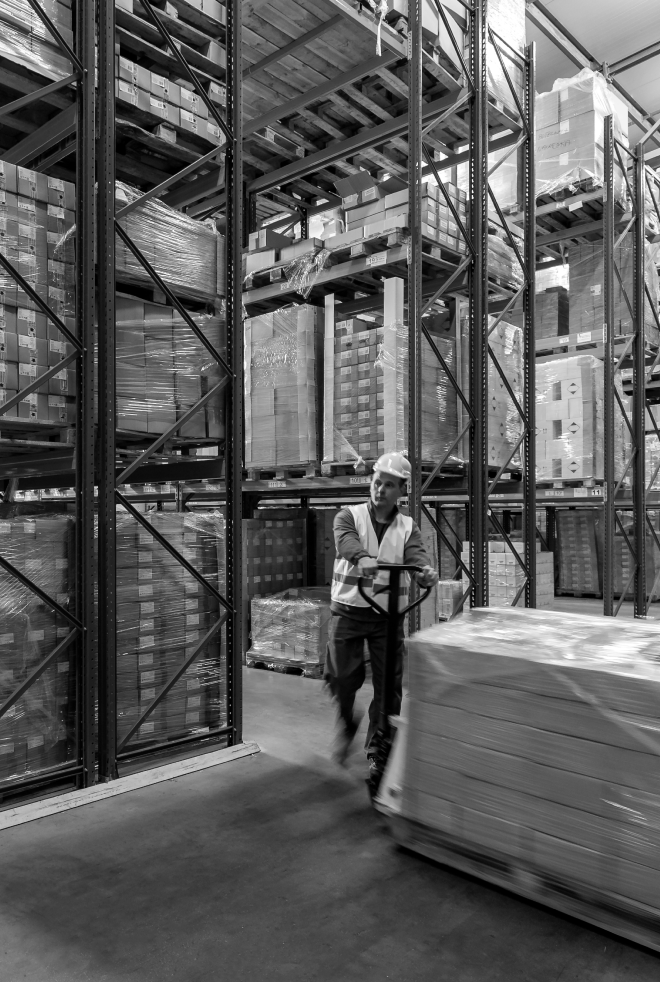
A warehouse that works without compromise – security, reliability and readiness for every challenge.
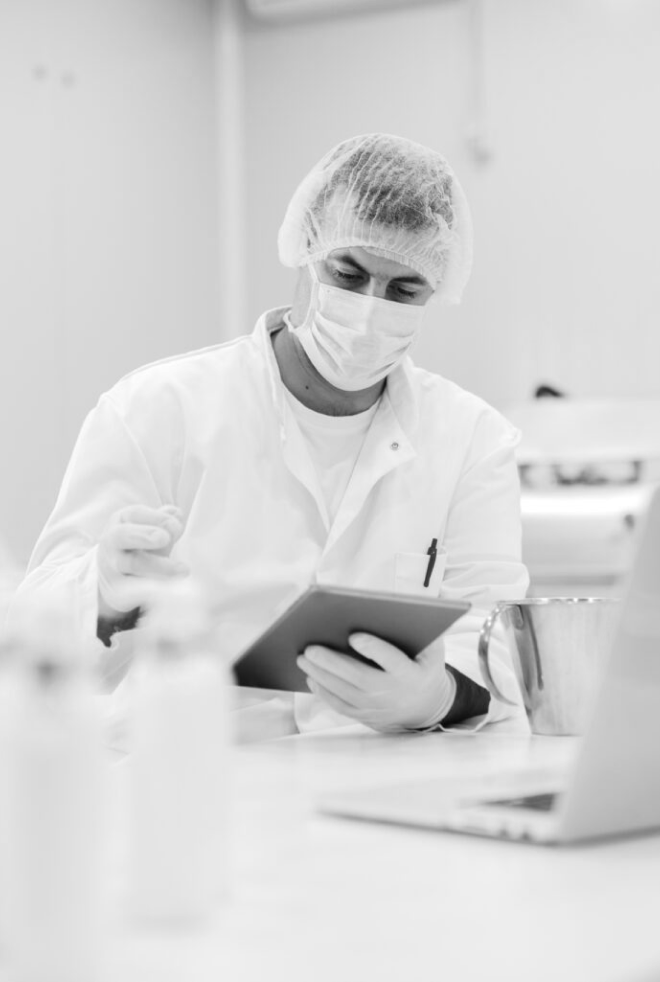
Modern laboratory
We create quality that distinguishes your brand
Advanced equipment for
the highest precision
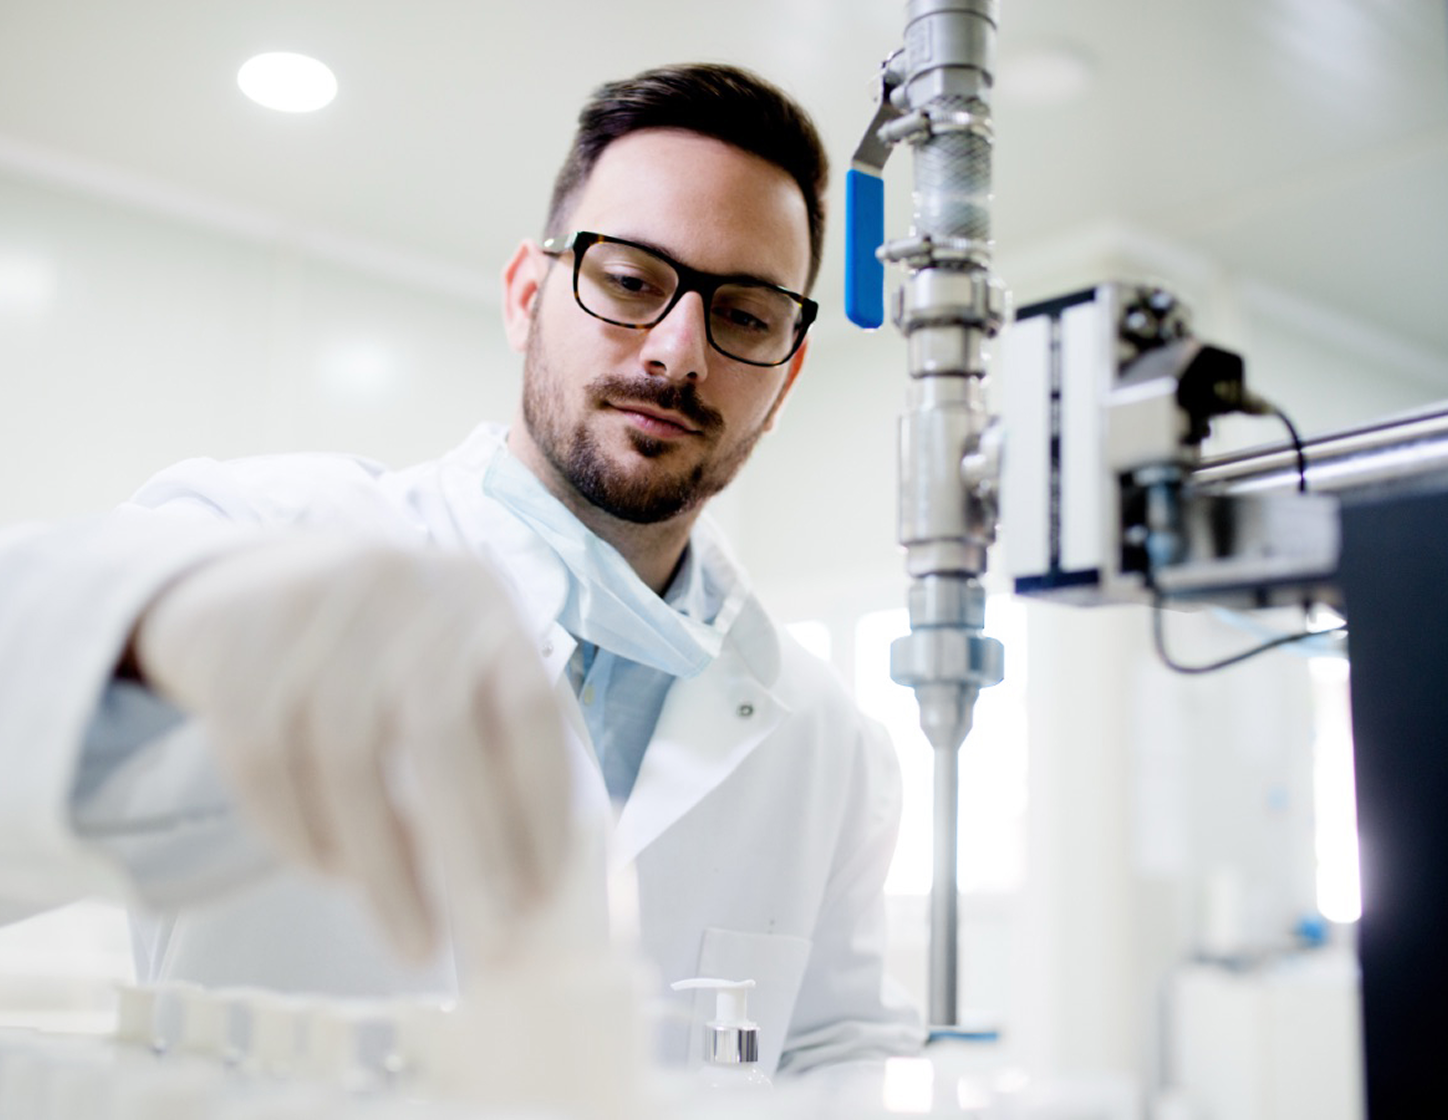
Our laboratory is the heart of innovation and quality control. Equipped in advanced equipment such as homogenizers, viscometers or luminometers, allows us to work with the highest precision. Thanks this ensures that your products not only meet industry standards, but also growing customer expectations.
Each recipe is tailored to your needs, from the ingredients active ingredients to fragrance compositions. We create formulas that are consistent with INCI requirements, based on raw materials from the best suppliers.
Quality appreciated
by the industry
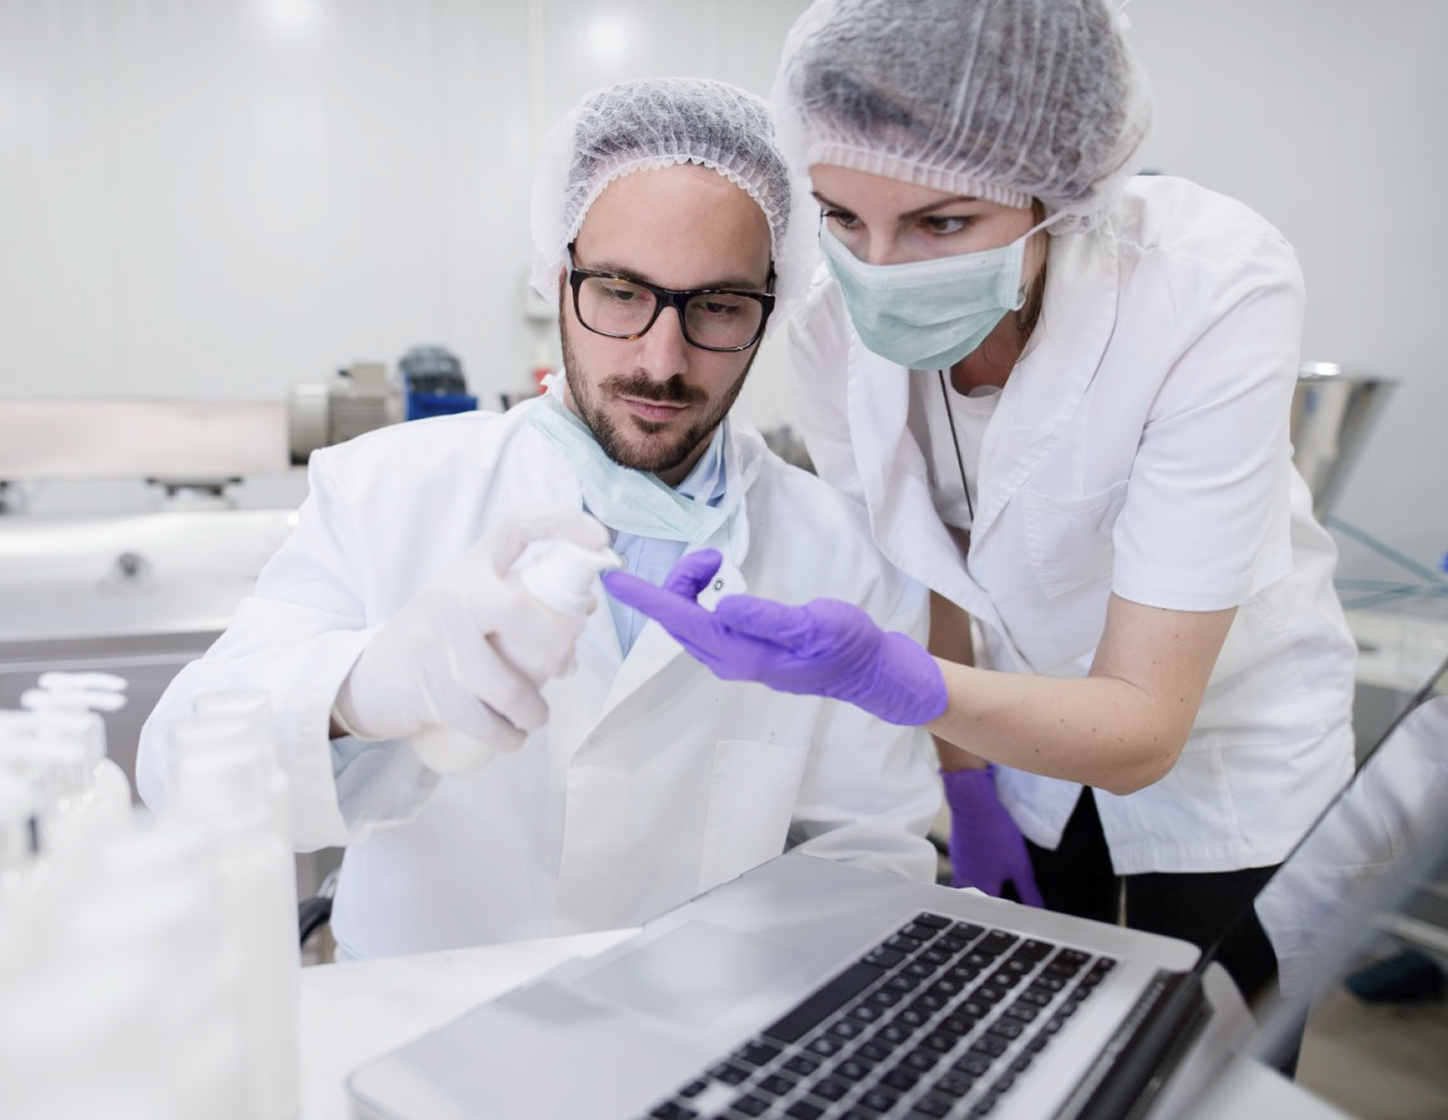
Quality control is our priority. At every stage of production, we conduct stability and compatibility tests. Packaging and safety of use. This is a guarantee that Your product will reach your customers in perfect condition.
Our quality has been recognized with numerous industry awards. We compare each product with an approved sample to ensure certainty that it meets the highest standards – your standards.
Production tailored
to your vision
We create quality that distinguishes your brand
Impressive production
capacity
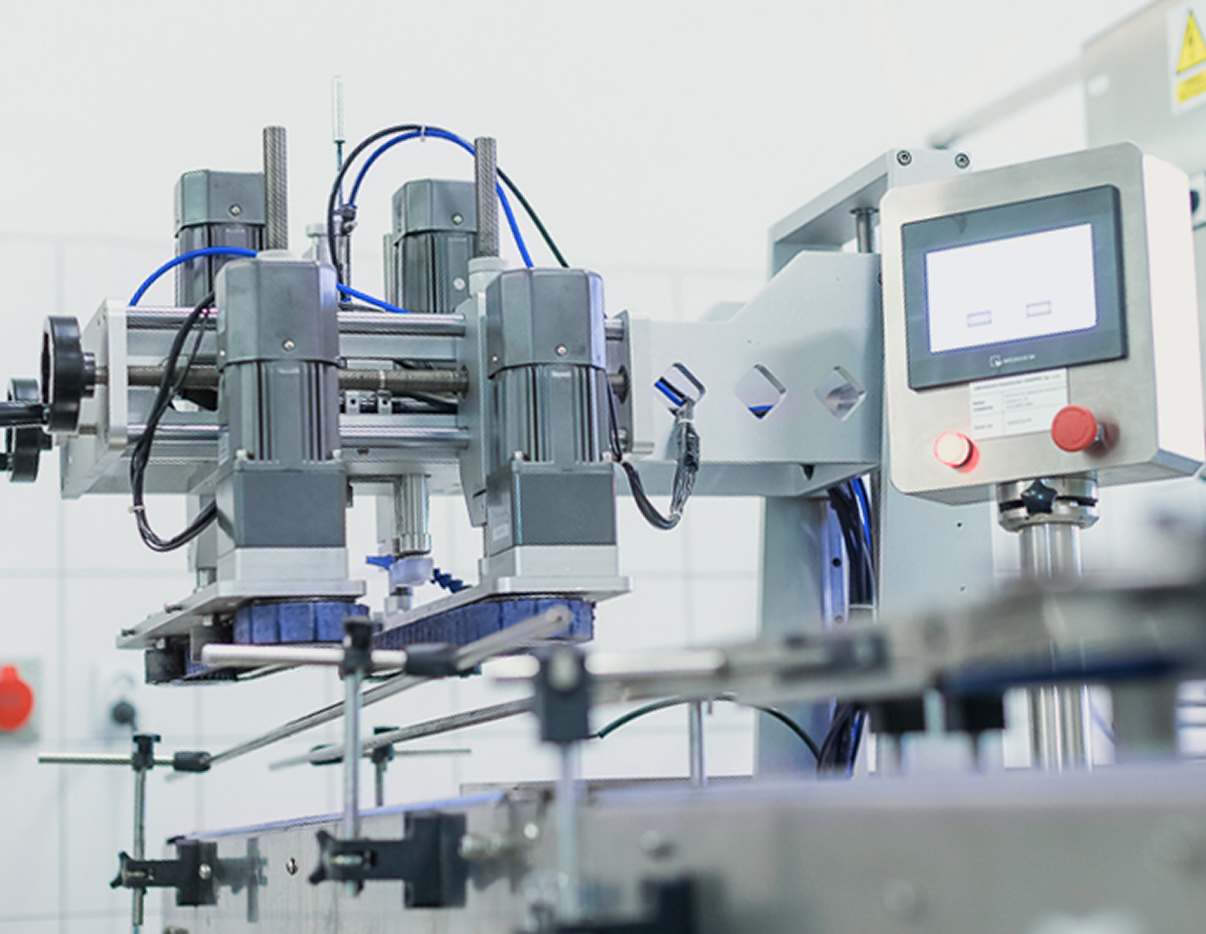
Thanks to modern production lines and advanced technology, we can produce up to 250 tons of cosmetics per month. We handle a wide range of packaging — from tubes and jars to sachets, vials, and canisters — adapting to the needs of your brand and customers.
We work in accordance with ISO standards, ensuring control at every stage — from formulation to finished product. We also offer recipe modifications to meet market needs.
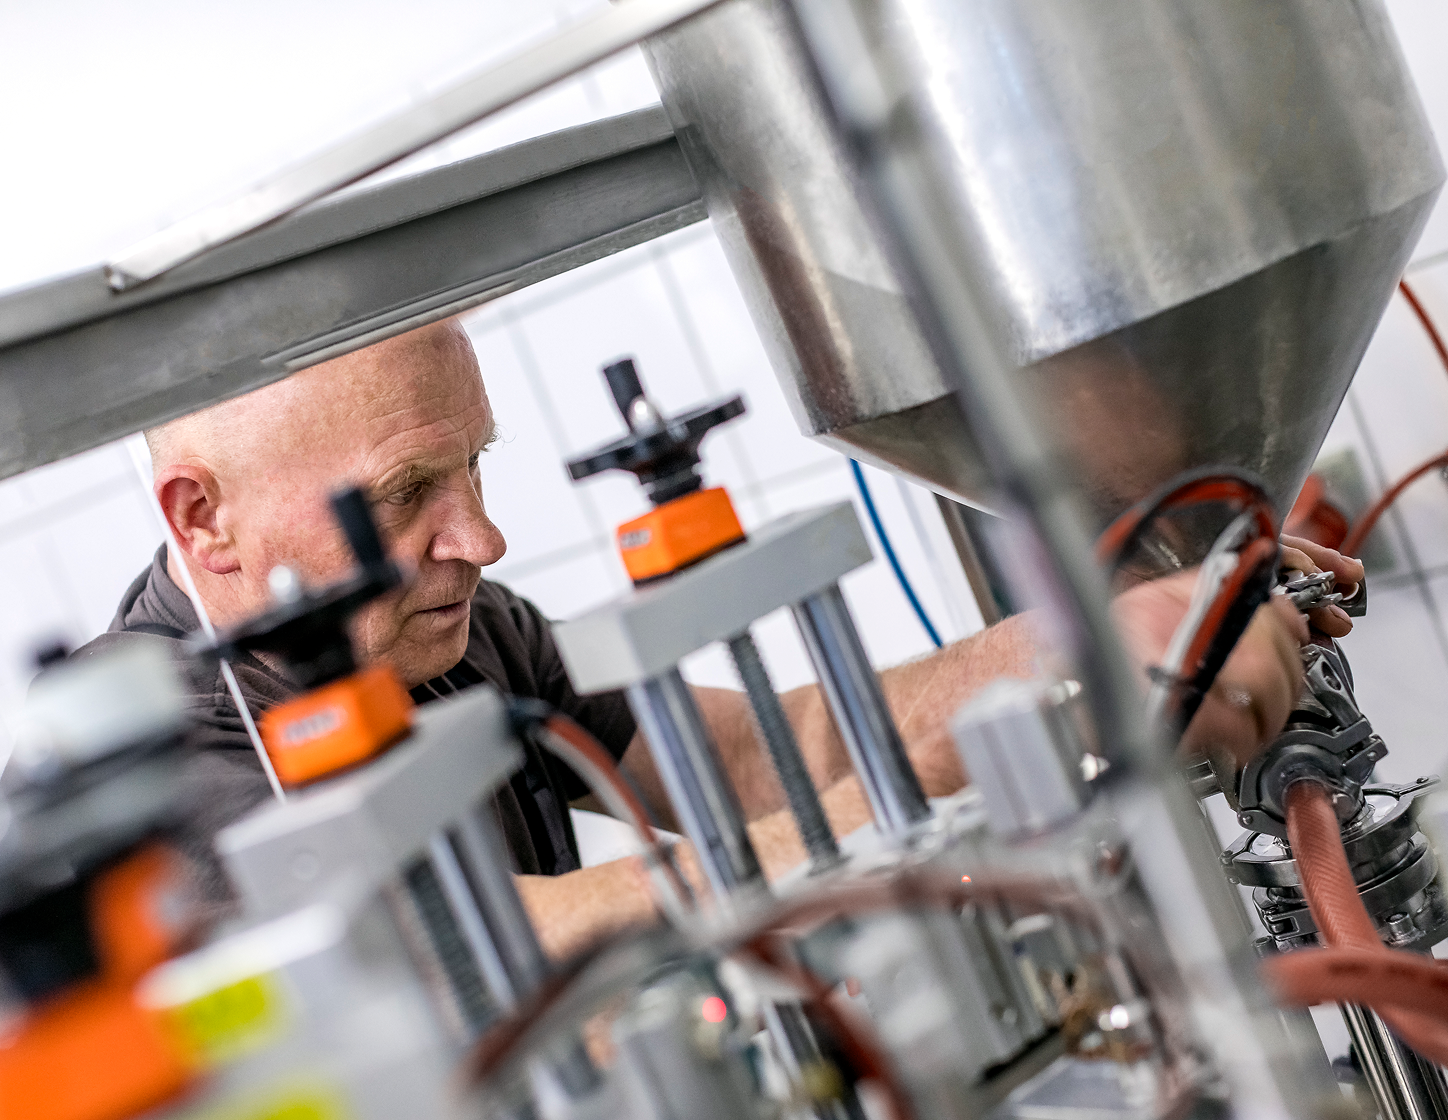
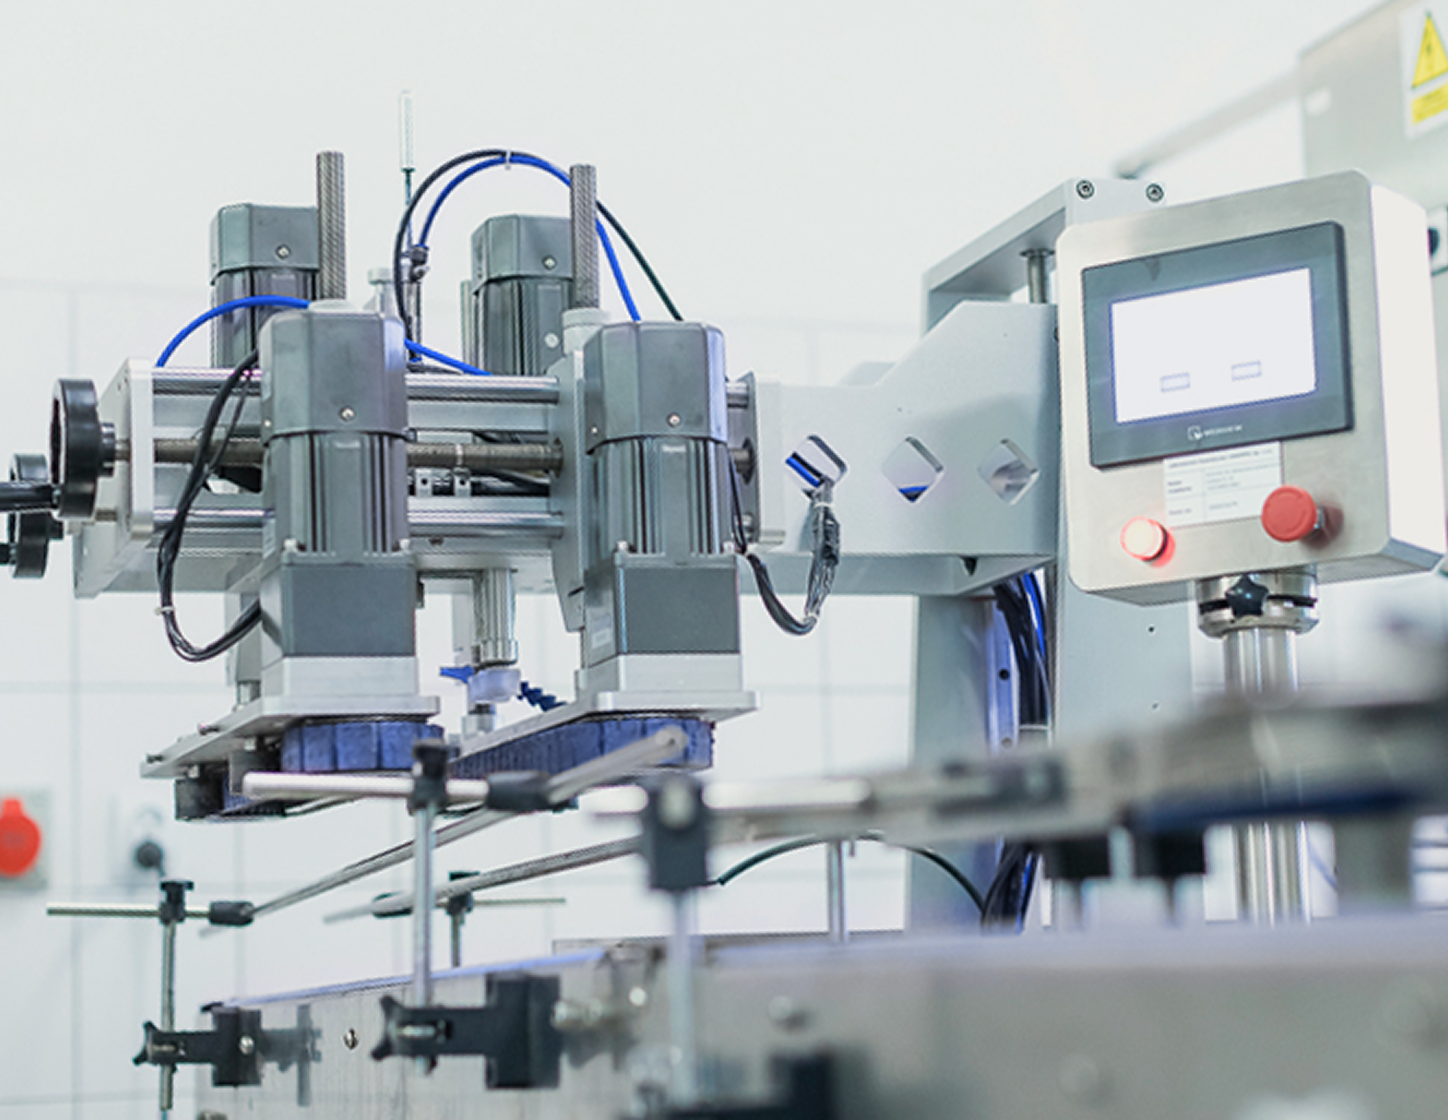
Modern machinery park
We have advanced machinery, including homogenizers, gelators, melters, mixers, tubing machines, sachet machines, a cooling tunnel, thermopacks, and labeling machines. A team of specialists oversees every stage of production, packaging, and labeling to ensure precision and reliability.
Regardless of the size of your order, we tailor our production process to your needs.
A form that adapts
to your product
A complete offering across all key product categories. Everything your brand needs, so you don't have to look for another supplier.
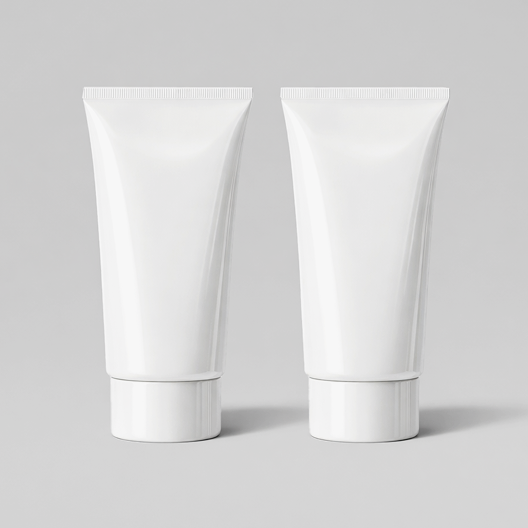
Tubes
Flexible and functional — perfect for creams, gels and daily care products.
Available in capacities from 5 to 250 ml.
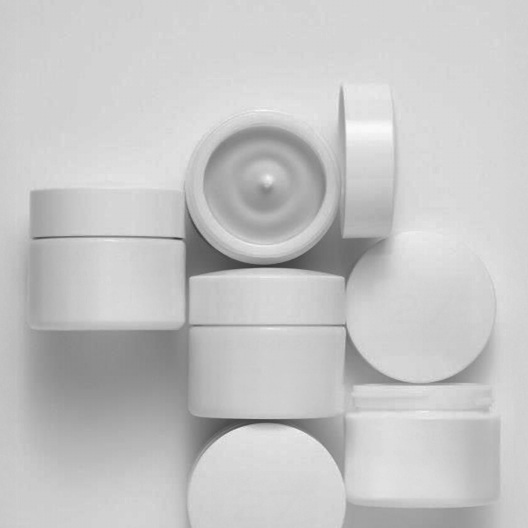
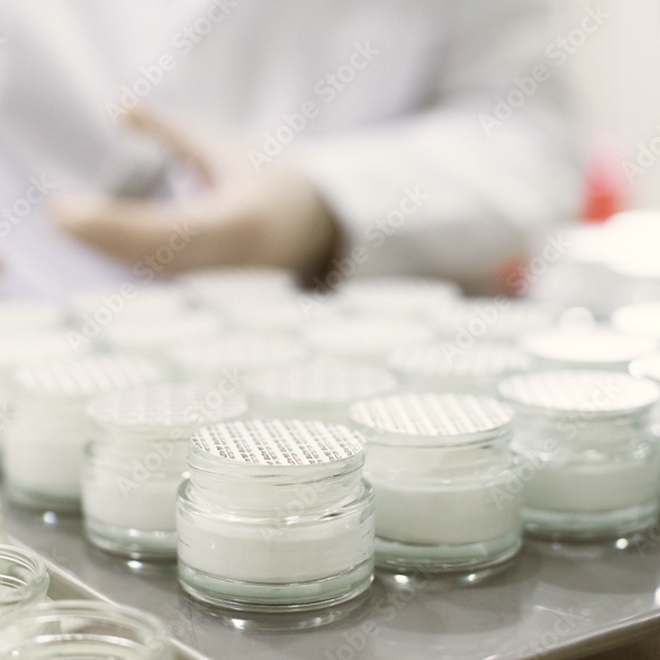
Jars
Aesthetic and solid — perfect for balms, masks and larger-volume products.
Available in capacities from 5 ml to 1 kg.
Bottles
Flexible and functional — perfect for creams, gels and daily care products.
Available in capacities from 5 to 250 ml.
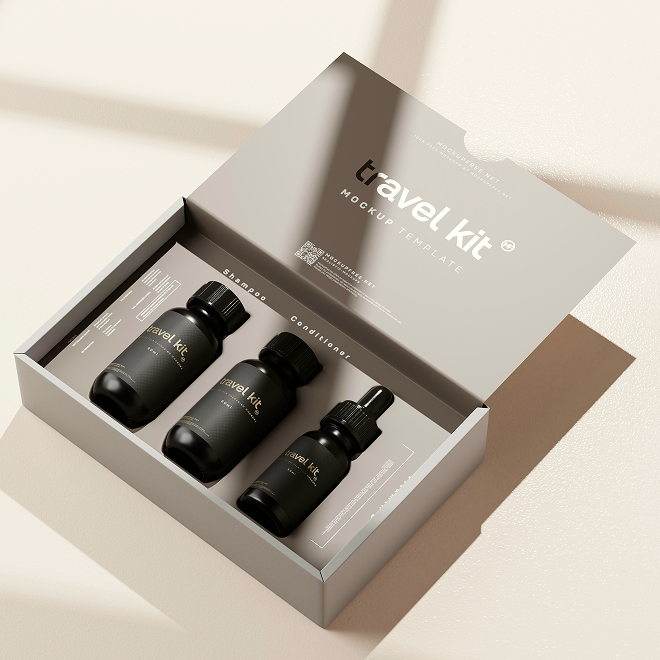
Dropper bottles
Aesthetic and solid — perfect for serums and loremipsum.
Available in capacities from 15 ml to 50 ml.
Sachets
Handy and compact — perfect for samples and products disposable.
Capacities from 1 to 20 ml.
Tube bottles
Combination of a tube and a bottle — functionality and convenience in one package.
Capacities from 30 to 50 ml.
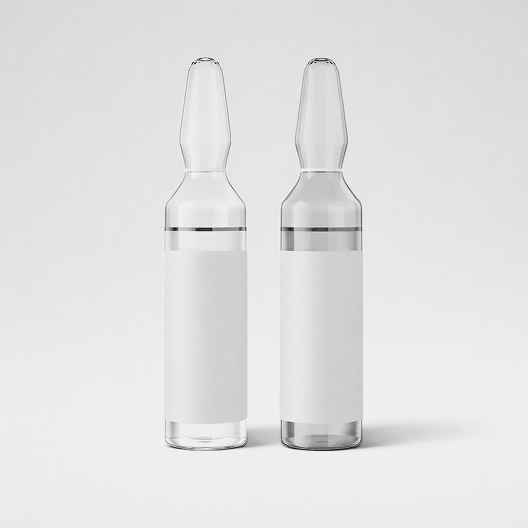
Vials
Precise and elegant — perfect for serums, oils and concentrates.
Capacities from 1 to 15 ml.
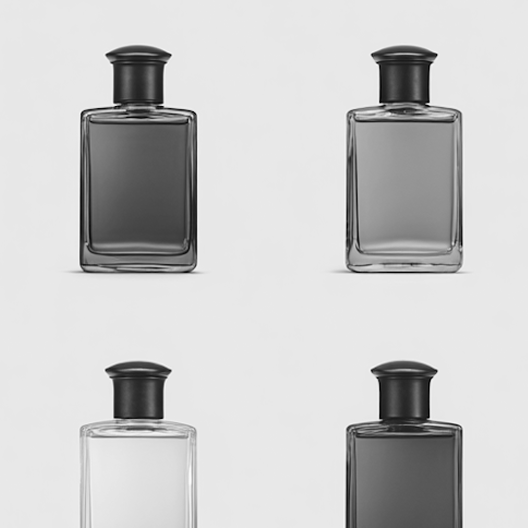
Glass bottles
Luxurious and durable — perfect for perfumes, oils and premium cosmetics.
Capacities from 5 to 200 ml.
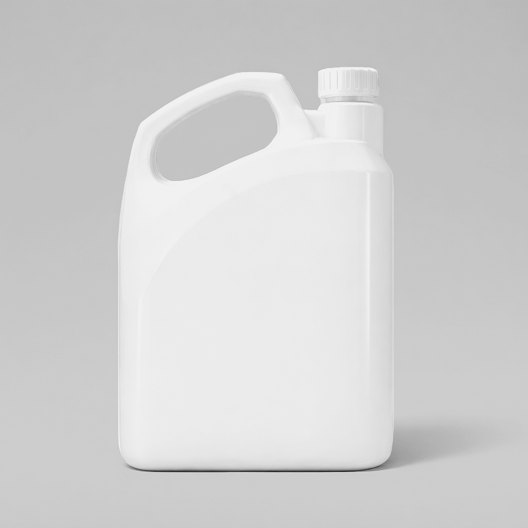
Canisters
Durable and spacious designed for large quantities of liquids and professional products.
Capacities from 1 to 20 l.
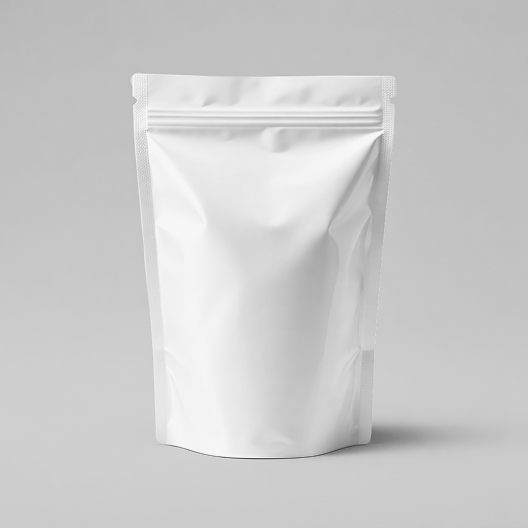
Doypacks
Convenient and modern — great for liquid and semi-liquid products.
Capacities from 20 ml to 1 l.
A warehouse
that guarantees
safety and efficiency
Duis autem vel eum iriure dolor in hendrerit in vulputate velit esse molestie consequat, vel illum dolore eu feugiat nulla facilisis at vero eros et accumsan et iusto odio dignissim.
Large warehouse space
We have 1000 m² of warehouse space and 1500 m² of production space. We plan to expand the warehouse to 2000 m² eventually. This allows us to provide efficient service to even the most demanding customers.
Our warehouse is equipped with forklifts, a reach truck, pallet trucks, an electronic floor scale, and a reverse osmosis water system with filters. We also have two ramps that allow for efficient loading and unloading of goods.
Safety at the highest level
Our warehouse is staffed by trained specialists with years of experience who oversee every stage of the work — from loading and unloading to the precise preparation of pallets for transport. Thanks to their knowledge and commitment, we complete orders with the utmost precision.
We work in compliance with occupational health and safety and fire protection regulations, and our qualified team oversees every technical detail.
See how we care for
your products
This short video reveals how our warehouse processes deliver the security, precision, and timeliness you need to grow your brand.

Schedule a call
Book a short 15 minute call to discuss your project, timelines, and the next steps toward production. No obligation.
Olga Wardziak
Sales Manager at Canexpol Group

Pick a time slot. Instant calendar invite.
Prefer email? Contact us
 Rated 4.8/5 based on verified Google reviews
Case studies
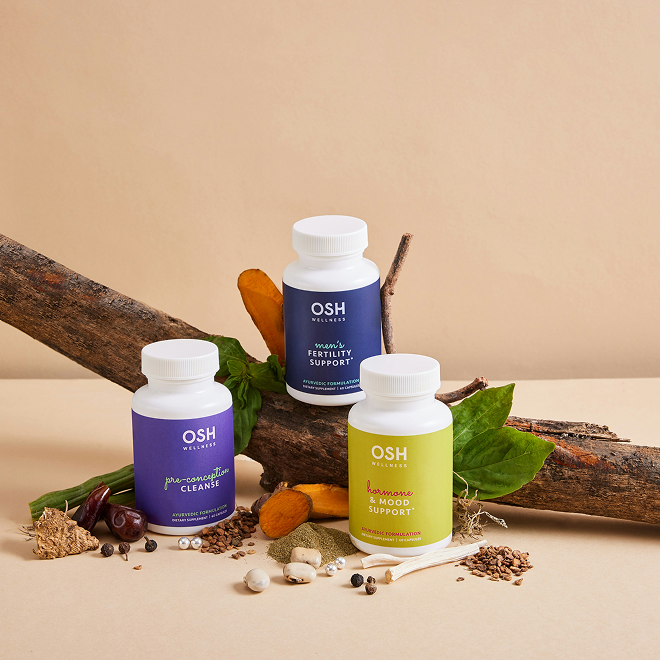
This is how our manufacturing process translates into predictable, manageable production for our clients.
Frequently asked
questions
Answers to the most frequently asked questions about our services, production process, and partnership model.
Thanks to our extensive network of verified suppliers and advanced monitoring systems, we ensure consistent supply of raw materials. When needed, we provide alternative sourcing options to prevent production delays.
Yes. We can discuss project scope, minimum quantities, packaging and production stages to find a realistic entry point.
Our team supports documentation, formulation review, testing coordination and manufacturing standards required for selected markets.
We help brands move from initial production runs to higher-volume manufacturing with adjusted processes and logistics.
We begin with a short discovery call, then define product scope, requirements, timeline, documentation needs and next production steps.